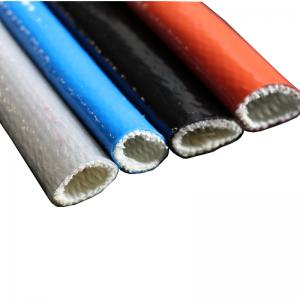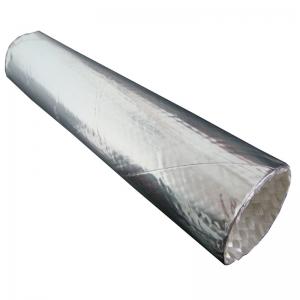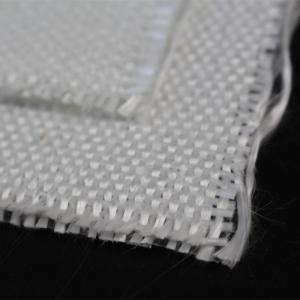
Saturated fiberglass sleeving is a braided glass fiber tube treated with a resin binder to help hold the yarns together during cutting and installation. For a production buyer, the useful question is how the finished sleeve behaves on the assembly line: whether a cut end stays manageable, whether the tube passes over the component, and whether it retains the required protection after service exposure.
BSTFLEX FGS-ST saturated braided fiberglass sleeve uses fiberglass yarn with an acrylic resin treatment. This guide describes a sample evaluation procedure; acceptance limits should be agreed for the intended assembly.
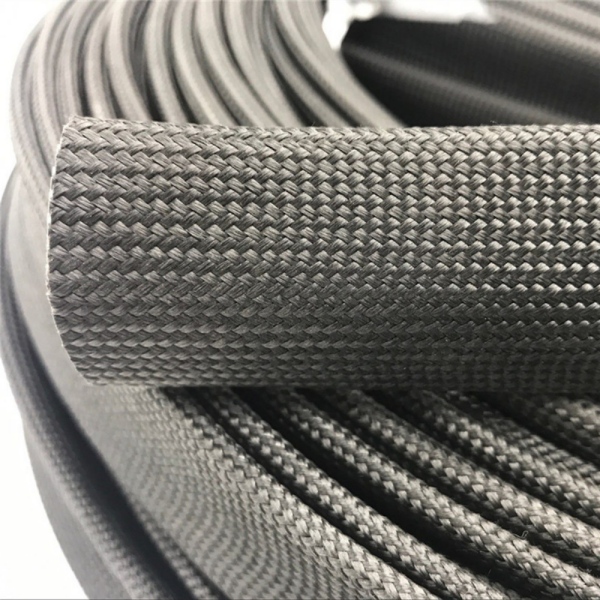
The treatment helps stabilize the braid and reduce loose fibers during handling. That can matter when operators cut many short pieces or push a sleeve along a cable or tube. It does not make every cut completely free of loose fibers, and it should not be taken as proof of a sealed, waterproof surface.
The condition of the glass braid and the condition of the binder are separate inspection points. For a heated installation, ask how the resin finish behaves during initial exposure and subsequent service. A temperature figure for the fiber does not establish that the original surface finish, flexibility or resistance to handling will remain unchanged at that temperature.
Begin with the proposed production size and thickness. Use the cutting tool intended for the job; the product page identifies scissors as a cutting option. Keep the blade condition and cutting method consistent when comparing samples. Measure the sleeve without stretching it, and record whether the production length refers to the relaxed cut piece or the installed coverage.
Inspect the cut immediately, then after normal handling. Photograph the same end before installation and after pulling the sleeve into place. Look for yarns separating from the braid, loose strands projecting into a connector area and changes in end shape. A freshly cut sample alone will not show what happens after repeated handling.
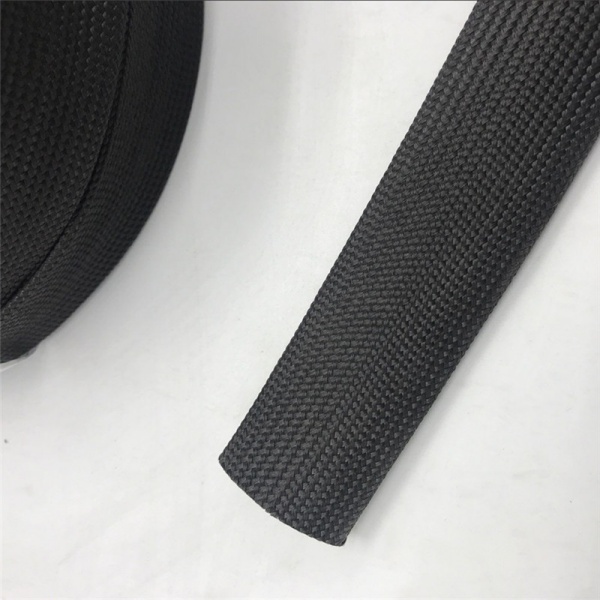
Use the largest outside dimension the sleeve must pass, including fittings, connector shoulders or local changes in tube diameter. Nominal sleeve ID is a starting point; the sample determines whether the finished construction passes without excessive force or damage.
Observe where operators grip the tube. Pulling hard on one end can change the shape of a braid and affect the length covering the component. Mark the required coverage on the assembly and check it again after the sleeve is positioned and retained. Include bends and clamps in the trial rather than testing only a straight section.
| Inspection point | What to record | Decision before production |
|---|---|---|
| Cut end | Fraying and loose fibers before and after handling | Agree an acceptable end condition using a reference sample or photograph |
| Fit over obstacles | Maximum passing dimension, installation effort and visible damage | Confirm size and assembly sequence |
| Installed coverage | Covered length, bunching at bends and movement at the ends | Set cut length and retention details |
| Contact with hardware | Rubbing locations and clamp pressure | Adjust routing or define a representative wear test |
| After heat exposure | Binder condition, flexibility, braid integrity and end stability | Approve the finished assembly against its service requirements |
Define the heat source, exposure duration and whether heating is continuous or cyclic. State whether the sleeve touches the hot surface or sits nearby. Where the purpose is thermal protection, measure the protected component under the intended operating conditions and compare the result with that component's allowable temperature.
If fluid exposure is relevant, identify the actual fluid, temperature and contact duration. A general chemical resistance description cannot establish compatibility with every cleaner, hydraulic fluid or process chemical. Include the intended cleaning method in the sample evaluation when the sleeve will be cleaned in service.
For applications with a specified electrical requirement, request data for the finished construction and applicable test method. Do not select a dielectric rating from the word fiberglass. Similarly, hose burst containment and direct flame protection require their own evidence; they are not established by passing a cut-end or abrasion check.
Keep the approved sample together with the agreed inner diameter, thickness, cut length, color and packaging. Record any end treatment and the method used to inspect it. If cut pieces will be supplied in bulk, assess how the ends survive packing and removal from the package, not just a single hand-prepared specimen.
The FGS-ST product page offers thickness, length and packing options on request. Send those requirements with the annual quantity and trial quantity so that the quotation corresponds to the same construction you intend to approve. Confirm current minimum order quantity in the quotation.
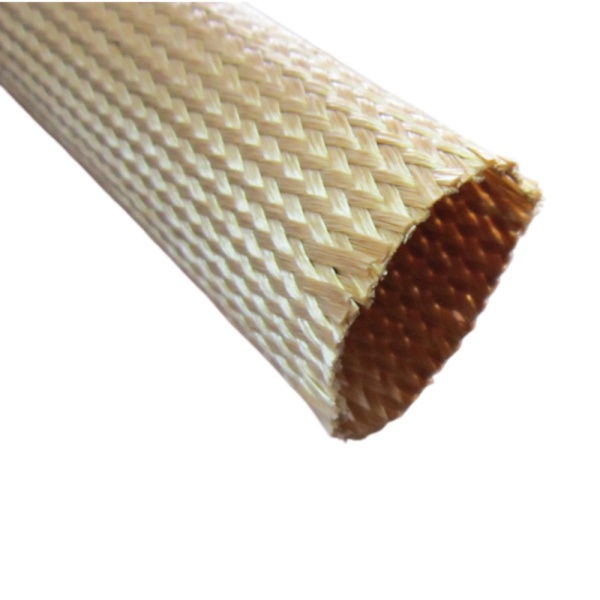
No. The treatment is intended to reduce fraying and improve handling stability. Cutting, repeated manipulation and installation over rough parts can still disturb the braid. Define acceptable cut-end quality for your process.
Do not assume so. Where vibration or servicing can move the sleeve, evaluate the retention method on the assembly. Confirm the suitability of any added tape, band or other termination for the temperature and adjacent component.
Yes, when it will operate in a heated environment. Inspect the braid and finish after the representative exposure, then repeat any handling or flexing expected during maintenance. The new sample's appearance alone is insufficient for that approval.
Provide the component diameter, largest installation obstacle, required coverage, available space, exposure conditions and quantity. Include photographs of bends and retaining points. For BSTFLEX sample development, Anhui Parker New Material Co., Ltd. can review these details against the proposed FGS-ST construction.
See the saturated fiberglass sleeve specifications to identify a starting size for your trial.

 English
 français
 Deutsch
 русский
 italiano
 español
 português
 Nederlands
 العربية
 日本語
 Türkçe
 Polski
 Tiếng Việt
 slovenský
 Indonesia